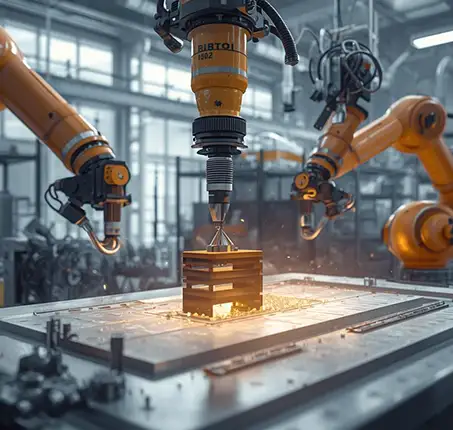
Material efficiency in DED refers to how effectively Directed Energy Deposition converts supplied metal powder or wire into deposited material and usable finished components. This metal additive manufacturing process can reduce waste by placing material where it is needed instead of removing large amounts from solid metal stock.
For aerospace, defense, and energy manufacturers working with expensive alloys such as titanium and Inconel, material utilization directly affects production costs.
Wire fed DED can achieve high feedstock utilization, while powder based DED experiences losses that depend on powder delivery, melt pool conditions, and deposition parameters.
Understanding these differences helps manufacturers evaluate material consumption, production efficiency, and the cost of manufacturing or repairing industrial components.
That means every piece you make can cost you up to hundreds of dollars. So even the smallest mistakes can be detrimental to the business.
Nowadays, factories are struggling because the price of metal has surged, alongside rising energy costs and growing environmental regulations. Expensive alloys are not just used for aesthetics; they are used to meet industry requirements for aerospace, defense, and engineering.
This is why Directed Energy Deposition is so popular among manufacturers. It helps them achieve material efficiency, so expensive metals don’t go to waste.
What Is Material Efficiency in Directed Energy Deposition?
When you look at an airplane, how do you think it was built? How were the individual parts created and put together? Well, believe it or not, there was a time when the parts were carved out like statues from stone. Not only was this inefficient and time-consuming, expensive material would get wasted in the process.
Manufacturing methods have come a long way since. Now you can draw the part you want, line by line, using metal. This process is called Directed Energy Deposition (DED), and it guarantees material efficiency.
But what is material efficiency?
Material efficiency in Directed Energy Deposition measures how effectively a manufacturing process uses metal feedstock. Two useful measurements are deposition efficiency and finished part material utilization.
Deposition efficiency compares the mass of metal successfully deposited with the total amount of feedstock supplied. Finished part material utilization considers how much of the starting material remains in the component after machining and other processing.
DED can improve material use by depositing metal powder or wire close to the required component geometry. However, losses may occur through powder overspray, spatter, process instability, rejected builds, and finish machining.
Actual material savings depend on feedstock type, machine configuration, process parameters, and component geometry.
. Manufacturing methods like DED create the exact shape you want by feeding metal powder or wire through a nozzle to achieve precision. The process can best be described as adding frosting onto a cake, but it’s metal, and you’re building a critical component for an airplane.
DED vs CNC Machining for Material Waste Reduction
Here’s how traditional manufacturing worked:
- You start big.
- Cut away the excess.
- Throw out the material you cannot use.
The problem with that system is that when you begin with a large metal block, you can end up with 80% of it as scrap. That metal could be expensive, like titanium.
Not to mention, this process is time-consuming. Delivering a mission-critical component can take weeks, if not months, to repair or duplicate..
In comparison, Directed Energy Deposition adds metal layer by layer instead of subtracting it. This process creates less scrap, lowers material costs, and is far more efficient. The only material you use is what is being deposited onto the build path and melted using precise lasers.
Directed Energy Deposition can reduce material waste compared with machining certain components from solid metal blocks. CNC machining removes material from a larger workpiece, while DED adds metal powder or wire along programmed deposition paths.
This difference is especially relevant when manufacturers produce near net shape components using expensive alloys.
However, DED does not eliminate material losses. Powder may miss the melt pool, deposited parts may require machining, and some builds may need additional processing or rejection.
Wire fed DED can achieve high deposition efficiency under suitable conditions, while powder fed systems have more variable material capture rates.
For the most useful comparison, manufacturers should evaluate material utilization, finished part weight, production time, machining requirements, and total manufacturing costs.
Key Factors That Influence Material Efficiency in DED
Material efficiency in DED goes beyond using less metal. This is a sophisticated system that allows you to build aerospace engines like a LEGO model, with every piece fitting perfectly.
Here are some factors that influence material efficiency:
High-Quality Powder or Wire
The reason why DED systems can create a complex part accurately from a design is because the wire or powder is melted consistently and predictably. The powder or wire is delivered on the build path with precision using a wire feedstock that minimizes spatter, fume, or minor losses around the melting pool.
Think of it like baking utensils that come in different shapes — once you deposit the dough in that shape, you get brownies in that precise shape.
Melt Pool Control
The melt pool is the tiny molten spot created by the laser. If the laser is too hot, it will burn the wire, or the puddles will be out of shape. If the laser is not hot enough, the wire will not melt right away, and the process will take longer than expected.
But thanks to DED, energy density stays consistent, so you can expect the melt pool to stay stable throughout.
Melt pool control plays an important role in DED material efficiency. Laser power, feedstock delivery rate, travel speed, and thermal conditions influence how effectively metal enters and solidifies within the deposition area.
An unstable melt pool can contribute to inconsistent bead geometry, porosity, incomplete fusion, and unnecessary material consumption.
Engineers adjust deposition parameters to maintain suitable melting conditions and consistent material placement. In powder fed systems, powder catchment efficiency also depends on nozzle alignment, powder flow, and the interaction between the powder stream and melt pool.
Proper process control can reduce defects and rework, but it cannot guarantee zero material waste.
In-Process Monitoring & Closed-Loop Systems
Let’s say something does go wrong — what do you do? The great thing about modern systems, such as FormAlloy’s DEDSmart® , is that they are equipped with feedback tools such as live visibility and playback. This allows you to watch in real time, and if something goes wrong with the melt pool, it will auto-correct for the best results.
Why DED Is the Future of Smart Manufacturing
Material efficiency is quickly becoming the backbone of smart manufacturing. Seeing the rising price of metal and how sustainability regulations are becoming more strict, the global supply chain needs smart manufacturing solutions now more than ever. This is exactly why industries like aerospace, defense, energy, and manufacturing are relying so heavily on FormAlloy’s Directed Energy Deposition systems.
If you are ready to transform your material efficiency with the next-gen DED solutions we have to offer, contact us for a demo.
Wire DED vs Powder DED Material Utilization
Wire and powder Directed Energy Deposition systems use different metal feedstock delivery methods, which influence material efficiency.
Wire fed DED delivers continuous metal wire into the deposition area. Under suitable processing conditions, a large proportion of the supplied wire can become deposited material. However, wire feeding stability, trimming losses, and finish machining still affect overall material utilization.
Powder fed DED delivers metal particles into a melt pool. Some particles may not enter the molten region, resulting in overspray and reduced powder catchment efficiency.
Powder utilization depends on nozzle design, particle characteristics, feed rate, laser settings, and deposition geometry.
Manufacturers should compare both methods using measured feedstock consumption, deposited mass, finished part weight, surface finish requirements, and production costs.
How to Measure Material Efficiency in DED
Manufacturers can measure DED material efficiency by comparing the amount of feedstock supplied, the amount successfully deposited, and the final usable component mass.
Deposition efficiency measures the proportion of supplied feedstock that becomes deposited metal.
Deposition Efficiency (%) = (Deposited Metal Mass ÷ Supplied Feedstock Mass) × 100
Finished part material utilization measures how much starting feedstock remains in the usable finished component.
Material Utilization (%) = (Finished Part Mass ÷ Starting Feedstock Mass) × 100
In aerospace manufacturing, engineers also use the buy to fly ratio to compare purchased material with the mass of the finished component.
Buy to Fly Ratio = Purchased Material Mass ÷ Finished Component Mass
A lower buy to fly ratio generally indicates that less starting material is required for the finished aerospace part.
When evaluating DED, manufacturers should account for substrate mass, machining allowances, powder losses, rejected builds, and any recovered material to ensure comparisons use consistent measurement boundaries.